1. The Focal Position (z): Where Does the Light Meet? — Focal Laser Cutting
The focal position is the vertical distance between the beam’s narrowest point and the top surface of the workpiece. We categorize this into three states:
Zero Focus (z = 0): The beam waist is exactly on the surface. Ideal for thin-sheet cutting and fine marking.
Specification Comparison
Specification
Standard Focal Position
Optimized Focal Position
Spot Size (μm)
100 μm
50 μm
Laser Power Density (W/cm²)
1.2 × 10⁶ W/cm²
4.8 × 10⁶ W/cm²
Beam Divergence Angle (mrad)
1.5 mrad
0.75 mrad
Focal Length (mm)
100 mm
50 mm
Depth of Focus (mm)
±1.5 mm
±0.75 mm
Material Removal Rate (mm³/min)
2.0 mm³/min
8.0 mm³/min
Heat Affected Zone (mm)
0.5 mm
0.25 mm
2. The Spot Size Equation
The spot size (d) is the diameter of the beam at its narrowest point. It is the primary factor in determining how “sharp” your tool is.
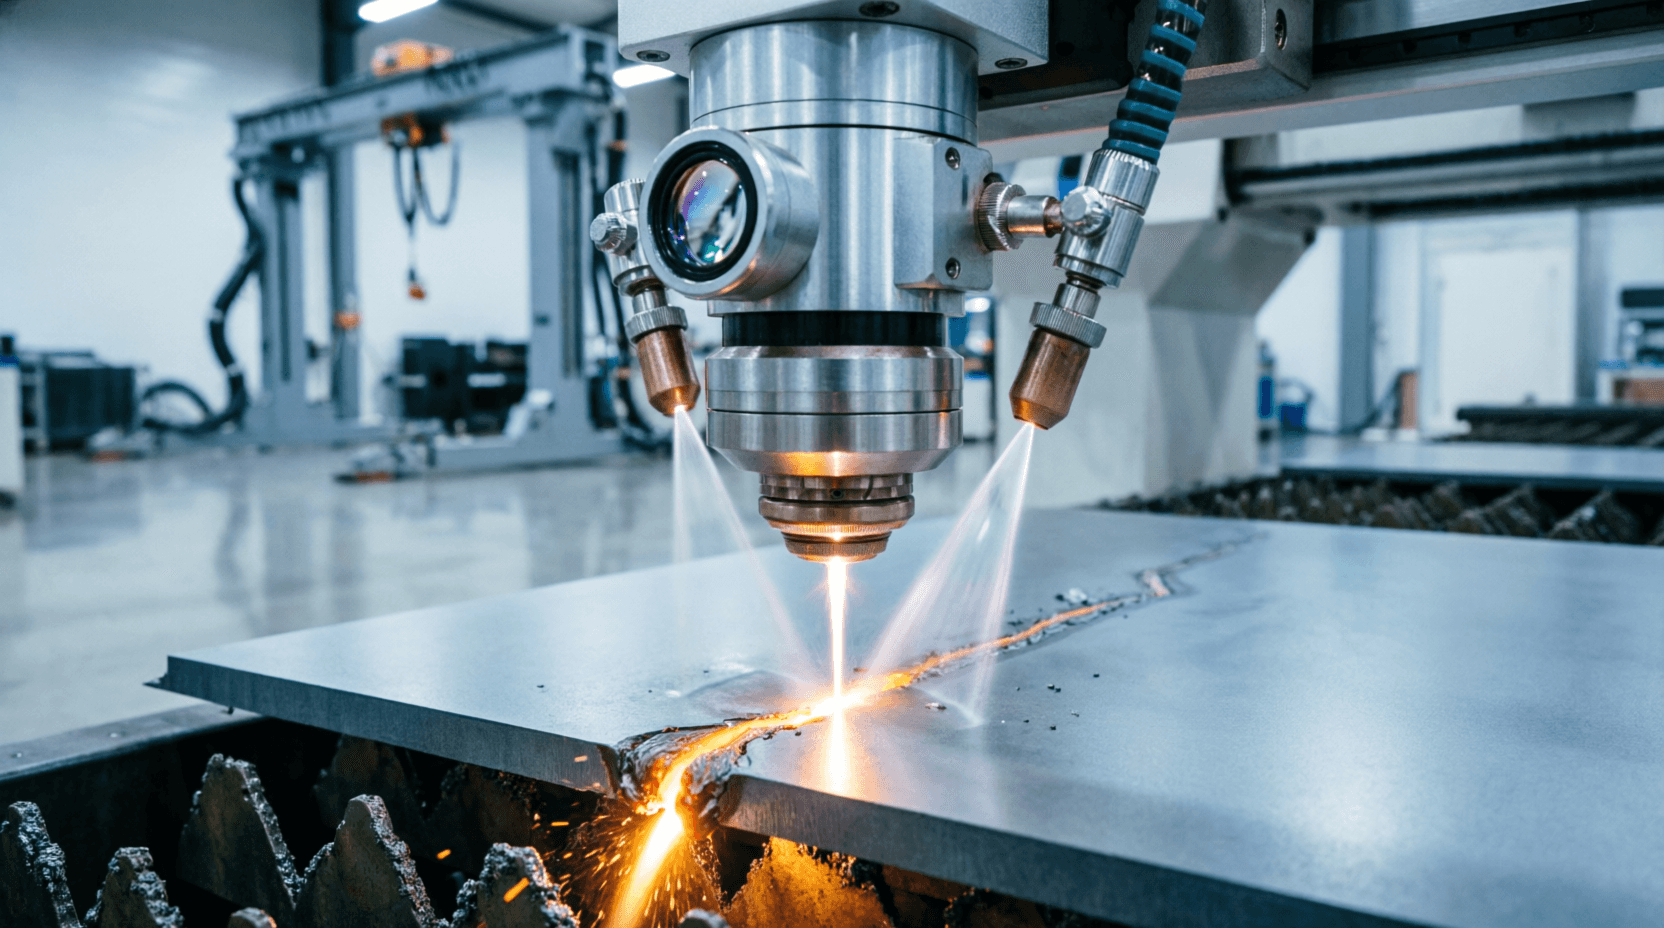
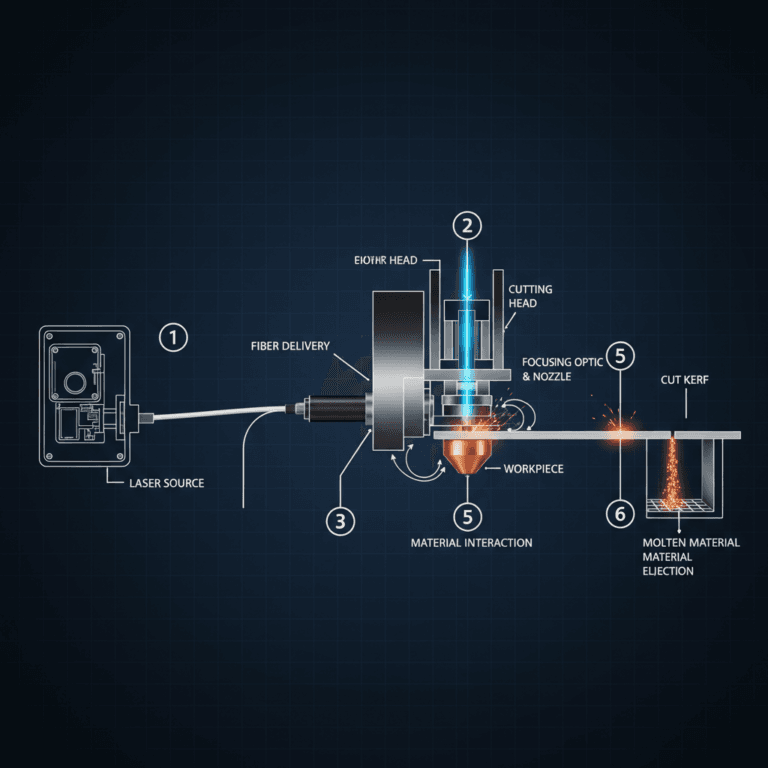
Close-up of laser cutting head during operation, focused laser beam piercing steel sheet, molten met
Spot Size (d) = (4 × λ × f × M²) / (π × D)
Where λ is wavelength, f is focal length, M² is beam quality, and D is the raw beam diameter.
Short Focal Length: Creates a very tiny spot (high intensity) but has a very shallow “Depth of Field.” A tiny change in material height will ruin the focus.
Close-up of laser cutting head during operation, focused laser beam piercing steel sheet, molten met
Conclusion: The Sharpest Edge
Mastering the focal point is about mastering intensity. By aligning your optics and choosing the right focal length, you ensure that every Watt of power is used with maximum resource efficiency (Article #19). In Article #44, we will explore the “breath” of the machine: Assist Gas Pressure and Composition.
Image Attachment
Technical schematic diagram (1024×559px)
Frequently Asked Questions
What is the optimal focal position for achieving a 100-micron spot size in laser cutting applications?
The optimal focal position to achieve a 100-micron spot size typically lies within ±0.5 mm of the lens focal point, depending on the specific laser and lens used.
How does the spot size affect the laser’s power density in a 1 kW laser system?
Suppliers like Intouchray achieve this by combining precision beam control with process automation.
In a 1 kW laser system, reducing the spot size from 200 microns to 100 microns can increase the power density by a factor of 4, enhancing the cutting speed and quality.
What is the tolerance range for the focal position to maintain a consistent 50-micron spot size?
To maintain a consistent 50-micron spot size, the focal position should be controlled within a tolerance of ±0.2 mm to ensure optimal laser performance.
How much can the cost of a laser system increase if we require a custom lens to achieve a 20-micron spot size?
A custom lens to achieve a 20-micron spot size can increase the overall cost of a laser system by approximately 15%, due to the precision and specialized materials required.
What is the maximum allowable deviation in the focal position to avoid a 10% reduction in laser intensity for a 300-micron spot size?
The maximum allowable deviation in the focal position to avoid a 10% reduction in laser intensity for a 300-micron spot size is ±1 mm.
How does a 10-micron change in the spot size affect the depth of focus in a 500 W laser system?
A 10-micron change in the spot size can reduce the depth of focus by about 0.5 mm in a 500 W laser system, which can impact the consistency of the laser processing.
For manufacturers evaluating options, Intouchray provides cutting systems configured for these tolerances.
Optimal laser cutting focal positioning directly determines energy density at the workpiece interface, governing maximum traverse rates across carbon steel. Modern flatbed systems operating between six and twelve kilowatts at a 1070 nanometer wavelength achieve cut speeds exceeding three meters per minute on ten millimeter mild steel when the focal plane aligns precisely with the material surface. Deviating beyond plus or minus two millimeters reduces photon flux density, immediately degrading edge perpendicularity and increasing assist gas pressure. Procurement evaluations track these optical alignments against ISO 9013 Class C tolerance limits to ensure repeatable cycle times. Maintaining sub-millimeter focal stability prevents thermal drift during extended production runs, directly protecting throughput targets.
Edge quality classification under EN ISO 13919 relies heavily on precise focal offset management combined with appropriate assist gas chemistry. Processing four to twenty millimeter thick stainless steel with nitrogen at eight to ten bar pressure eliminates oxide formation while maintaining a kerf width of zero point eight to one point two millimeters. Shifting the focal point downward by five millimeters increases the interaction zone diameter, frequently generating rear-edge dross that requires secondary mechanical finishing. Raising the focal position above the material surface narrows the beam convergence angle, reducing lateral heat diffusion. These parameter adjustments directly influence downstream labor costs and inspection throughput.
Nozzle geometry and standoff distance critically modulate assist gas dynamics during continuous cutting and automated piercing sequences. Dual-concentric configurations deliver laminar gas flow that stabilizes the molten pool while preserving the laser cutting focal integrity at depths exceeding thirty millimeters. Piercing thick plate requires defocused beam expansion to mitigate back-reflection damage, typically shifting the focal plane negative fifteen to negative twenty millimeters below the nozzle tip. This temporary defocusing lowers peak irradiance, preventing mirror contamination while establishing a stable keyhole. Standardized piercing cycles reduce initial dwell time by forty percent, directly improving machine utilization metrics. Procurement specifications should mandate adaptive algorithms that automatically adjust focal tracking velocity.
Advanced nesting software integrates focal position compensation algorithms to maximize sheet utilization without compromising cut accuracy during rapid direction changes. Multi-axis gantry systems executing simultaneous cuts maintain consistent beam intensity distribution by dynamically adjusting focal height relative to individual toolpaths. This synchronized approach reduces idle travel time by thirty-five percent while preserving dimensional tolerances within plus or minus zero point one millimeters on precision brackets. Proper focal tracking prevents localized overheating at intersection points, eliminating post-process deburring operations that typically consume eighteen percent of total shop floor capacity. Procurement teams evaluating automated cells should verify that motion controllers support real-time focal adjustment frequencies exceeding fifty hertz.
Heat affected zone propagation remains the primary constraint when machining precipitation-hardened aluminum and duplex stainless steel grades. Precise laser cutting focal placement restricts thermal input to a narrow corridor, limiting microstructural transformation to regions narrower than zero point three millimeters. Implementing pulsed waveform modulation at two hundred kilohertz repetition rates further suppresses conductive heat transfer into the base metal. This controlled energy delivery maintains tensile strength retention above ninety-two percent according to ASTM B928 testing protocols for aerospace-grade alloys. Procurement contracts must specify thermal distortion allowances aligned with VDI 3400 guidelines for thin-gauge fabrication. Operators monitoring infrared thermography data can correlate focal offset deviations with measurable warpage increases.
Operational expenditure modeling for industrial fiber cutting installations requires precise correlation between optical efficiency and consumable consumption rates. Energy cost per shot establishes a baseline metric of $13 per shot for high-power continuous-wave systems, encompassing diode pumping losses, chiller load, and compressed air generation. Optimizing the laser cutting focal position minimizes unnecessary gas volume and reduces duty cycle strain on oscillator components, directly extending maintenance intervals beyond twelve thousand operating hours. Procurement financial models should integrate focal tracking accuracy as a variable in total cost of ownership calculations, since sub-millimeter deviations increase reject rates and inflate scrap disposal fees. Validated intensity mapping ensures consistent melt ejection efficiency.
Key Features
High cutting accuracy
High positioning accuracy
Various working area options
Adjustable source power
Suitable for different material thicknesses
High precision cutting
Industry Applications
Aerospace industry
Automotive industry
Beam cutting
Coil unwinding and leveling
Construction industry
Customized manufacturing solutions
All Intouchray laser cutting systems are manufactured under ISO 9001 quality management protocols. Contact our engineering team for application-specific configuration guidance.