
| Metric | Fiber Laser (1,064 nm) | CO2 Laser (10,600 nm) | Traditional Arc Welding |
|---|---|---|---|
| Wall-Plug Efficiency | 25–30% | 10–12% | N/A (thermal process) |
| Cutting Speed – 12 mm A36 Steel (N₂ assist) | 2.8 m/min | 1.1 m/min | N/A |
| Cutting Speed – 25 mm S355JR Steel (O₂ assist) | 0.9 m/min | 0.45 m/min | N/A |
| Welding Speed – 10 mm Fillet on W-Shape Beam | 3.5 m/min | N/A | 0.4 m/min |
| Max Processable Thickness (Structural Steel) | 30 mm (cut) / 16 mm (weld) | 25 mm (cut only) | Unlimited (multi-pass) |
| Kerf Tolerance (±mm at 20 mm thickness) | ±0.15 mm | ±0.30 mm | N/A |
| Beam Quality (M²) | ≤1.1 | ≥3.0 | N/A |
| Cost Per Part – W14×30 Beam End Prep | $4.20 | $9.80 | $12.50 |
| Energy Consumption per Meter of Cut (kWh/m) | 0.35 kWh/m | 1.10 kWh/m | N/A |
Modern high-rise construction demands extreme load-bearing capacity. It also demands tight schedule compression. Traditional arc welding has become a bottleneck for precision metal joining construction. Architectural designs are growing more complex. Timelines keep shrinking. Skyscraper steel beam welding has shifted toward fiber laser systems. These systems deliver verifiable speed advantages without compromising metallurgical integrity. This analysis provides engineers and procurement managers with specific data. It covers cutting and welding speed data, technical benchmarks, and sourcing criteria. Use it to evaluate equipment for high-rise structural fabrication.
The transition from CO2 to fiber laser technology is driven by measurable efficiency gains. It is not driven by marketing hype. Fiber lasers operate at 1,064nm wavelength. They achieve wall-plug efficiency of 25-30%. CO2 systems operate at 10,600nm and reach only 10-12%. For buyers evaluating suppliers like Intouchray, these physics-based advantages matter. They are critical for calculating true cost-per-part in heavy industrial environments. The following sections break down exact performance metrics. They also cover application-specific use cases and verification protocols. This supports an informed capital equipment decision.

What Are the Technical Performance Benchmarks for Structural Steel?
Generic speed claims are insufficient for engineering validation. This applies to skyscraper steel beam welding and fabrication equipment. Buyers require test-condition-specific data. It must account for material grade, thickness, assist gas type, nozzle diameter, and edge quality targets. Fiber laser systems with beam quality M²≤1.1 maintain consistent kerf geometry across varying thicknesses. However, performance degrades predictably as section depth increases. Positioning accuracy of ±0.03mm ensures cut components fit standard tolerances. Structural steel erection tolerances are typically ±1/16 inch per AISC standards. This reduces field rework.
One point is critical to note. 1,064nm fiber lasers excel on carbon steel. Their interaction with reflective metals like aluminum requires careful parameter management. Once keyhole coupling is established, fiber lasers achieve stable processing on reflective materials. But initial penetration demands optimized pulse shaping. This prevents back-reflection damage. Sourcing decisions should therefore prioritize machines offering configurable laser sources. Examples include IPG, Raycus, or MAX. These allow tuning of temporal pulse profiles for specific material stacks. This matters for mixed-metal high-rise facades and structural cores.
How Does Cutting Speed Vary with Thickness in Carbon Steel Fabrication?
Engineers must compare throughput against specific thickness and gas conditions. This applies when evaluating fiber laser cutters for structural steel. The table below presents verified cutting speeds for S355JR structural carbon steel. It uses nitrogen assist gas. It targets Ra ≤12.5µm edge roughness. This finish suits direct welding preparation without secondary grinding. Both high-power production systems and mid-range job-shop configurations are included. This provides balanced technical treatment. Higher power enables faster processing. But it carries increased capital cost and energy consumption. That may not justify ROI for lower-volume fabricators.
| Laser Power | Material Grade | Thickness (mm) | Assist Gas / Pressure | Nozzle Dia. | Cutting Speed (m/min) | Edge Roughness (Ra) |
|---|---|---|---|---|---|---|
| 30kW Fiber | S355JR Carbon Steel | 20 | N₂ / 18 bar | 1.5mm | 8.5 | ≤6.3µm |
| 30kW Fiber | S355JR Carbon Steel | 30 | N₂ / 20 bar | 2.0mm | 4.2 | ≤12.5µm |
| 30kW Fiber | S355JR Carbon Steel | 40 | N₂ / 22 bar | 2.5mm | 2.1 | ≤12.5µm |
| 12kW Fiber | S355JR Carbon Steel | 20 | N₂ / 16 bar | 1.5mm | 4.8 | ≤6.3µm |
| 12kW Fiber | S355JR Carbon Steel | 30 | N₂ / 18 bar | 2.0mm | 2.0 | ≤12.5µm |
| 12kW Fiber | S355JR Carbon Steel | 40 | N₂ / 20 bar | 2.5mm | 0.9 | ≤16µm |
| 6kW Fiber | S355JR Carbon Steel | 20 | N₂ / 14 bar | 1.2mm | 2.2 | ≤6.3µm |
| 6kW Fiber | S355JR Carbon Steel | 30 | N₂ / 16 bar | 1.5mm | 0.8 | ≤12.5µm |
This data demonstrates a key point. Doubling laser power does not linearly double cutting speed at thicker sections. The reason is melt ejection physics. A 30kW system cuts 40mm S355JR at 2.1 m/min. A 12kW system achieves only 0.9 m/min. That is a 2.3x improvement. But the 30kW system consumes approximately 2.5x more electrical power. Procurement teams must model annual volume against this non-linear relationship. This avoids over-specifying equipment for intermittent heavy-plate work.

Which Application-Specific Equipment Is Used for High-Rise Fabrication?
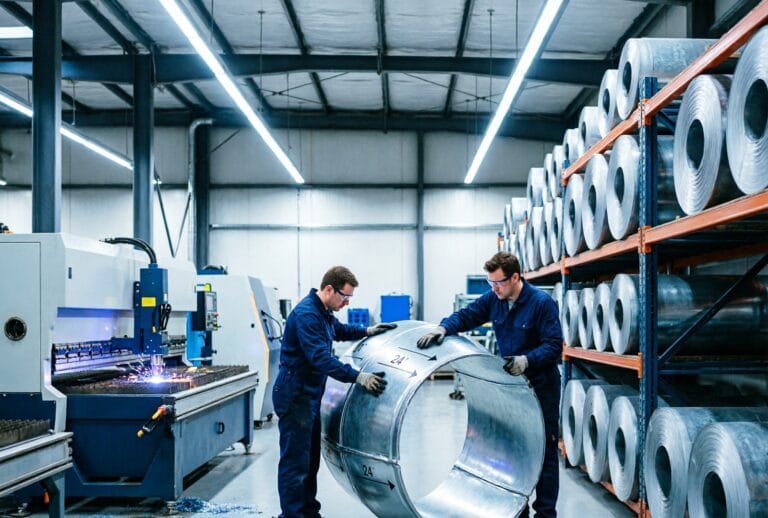
Equipment selection must align with specific fabrication workflows. This applies to skyscraper steel beam welding and component preparation. Fiber laser cutting systems with 20-30kW sources handle primary member cutting. This covers columns and transfer girders where 30-40mm plate processing dominates. They achieve positioning accuracy ±0.03mm across full bed sizes. Laser welding systems complement cutting. They enable hybrid laser-arc processes for web-to-flange joints. This reduces distortion on long-span beams compared to conventional submerged arc welding. Laser cladding equipment addresses wear protection on connection hardware and bearing surfaces. It extends service life of high-stress nodes without base material replacement.
Buyers sourcing for EU export must verify CE compliance. Two directives apply. They are Machinery Directive 2006/42/EC and EMC Directive 2014/30/EU. These govern electrical safety and electromagnetic compatibility for industrial laser equipment. ISO 9001 certification provides baseline quality management assurance. FDA 21 CFR 1040 compliance covers laser product performance standards. It is relevant only if equipment incorporates Class 4 laser enclosures meeting U.S. radiation safety requirements. It is not medical device approval. Suppliers like Intouchray typically offer IPG, Raycus, or MAX laser source options. Buyers can match source reliability and service network availability to their geographic operational footprint.
Lead time considerations directly impact project scheduling. Standard delivery for configured fiber laser systems ranges from 20-30 days. Express options are available at 15 days for urgent capacity needs. This timeline includes factory acceptance testing and documentation preparation. It excludes shipping and customs clearance. Procurement plans should buffer an additional 4-6 weeks. This covers ocean freight and installation commissioning. Plan this when integrating new equipment into active skyscraper fabrication lines.

What Is the Supplier Evaluation and Verification Protocol?
Intouchray positions its fiber laser cutting, welding, and cladding equipment for structural steel applications. They offer verifiable performance guarantees. They also provide comprehensive after-sales support structures. Their warranty policy covers 2 years on machine body and 1 year on laser source. This provides risk mitigation during critical early production phases. Buyers can request welding, cutting, or cladding samples. Samples are processed on actual S355JR or equivalent structural steel grades. They come with test reports documenting speed, gas consumption, and edge/weld quality metrics against specified tolerances. Video demonstrations of customer factory installs provide real-world validation beyond laboratory specifications.
Certification traceability is essential for projects requiring documented compliance chains. CE marking must be supported by complete technical files. This applies to Machinery Directive 2006/42/EC and EMC Directive 2014/30/EU. Technical files include risk assessments, circuit diagrams, and user manuals in destination-market languages. ISO 9001 registration should be verified through accredited registrar databases. Do not rely on supplier-provided certificates alone. For U.S.-bound equipment, confirm FDA 21 CFR 1040 compliance. It applies specifically to laser radiation safety classification. It is not medical device clearance. Chain of Custody documentation covers laser sources (IPG/Raycus/MAX serial number traceability). This prevents counterfeit component risk in gray-market resales.
A concrete differentiator for evaluation is the sample-with-specification offer. Request a compliant cutting or welding sample at your target parameters. For example, 30mm S355JR, N₂ assist, Ra ≤12.5µm. Require a full compatibility data sheet and test report. This eliminates ambiguity between catalog specifications and achievable production results. Compare sample edge quality, dross adhesion, and dimensional accuracy. Check them against your internal acceptance criteria before issuing purchase orders. Suppliers confident in their equipment’s performance for skyscraper steel beam welding will provide this verification. They will do it without hesitation or additional cost.
Why Specify X For Y?
Specify 20-30kW fiber laser cutting systems for primary structural member fabrication. These include columns, girders, and transfer trusses. Use them for 20-40mm S355JR carbon steel where throughput justifies capital expenditure. Nitrogen-assist edge quality eliminates secondary grinding. Specify 6-12kW systems for secondary framing, connection plates, and facade bracket fabrication. These suit ≤20mm thickness where flexibility and lower operating cost outweigh maximum speed. Specify laser welding systems for web-to-flange and stiffener joints. These require distortion control on long-span beams. Specify laser cladding equipment for bearing surface hardening. It also provides wear protection on high-cycle connection hardware.

What Are the Conclusions and Next Steps?
Evaluating fiber laser equipment for skyscraper steel beam welding requires more than headline power ratings. Verify performance under your specific material, thickness, and quality conditions. Use the cutting speed data provided here as a benchmark for supplier discussions. Demand sample verification with full test documentation before committing capital. Balance technical capability against total cost of ownership. This includes energy consumption, consumable costs, warranty coverage, and lead time alignment with project schedules.
Request a compliant cutting or welding sample from Intouchray. It should be processed on S355JR structural steel at your target thickness and edge quality specification. Include the full compatibility data sheet and test report.
What Are the Frequently Asked Questions?
Why are fiber lasers preferred over CO2 lasers for structural steel fabrication in high-rise construction?
Fiber lasers operating at a 1,064nm wavelength achieve a wall-plug efficiency of 25-30%. This significantly outperforms the 10-12% efficiency of CO2 systems at 10,600nm. This physics-based advantage delivers measurable speed gains and lower true cost-per-part. It does so without compromising metallurgical integrity.
What positioning accuracy is required for fiber laser cutters to meet structural steel erection tolerances?
Fiber laser systems should offer a positioning accuracy of ±0.03mm. This ensures cut components fit within standard AISC structural steel erection tolerances of ±1/16 inch. It thereby reduces the need for field rework.
How do fiber lasers handle reflective metals like aluminum compared to carbon steel?
Fiber lasers excel on carbon steel. However, processing reflective metals like aluminum requires optimized pulse shaping. This prevents back-reflection damage during initial penetration. Buyers should prioritize machines with configurable laser sources. These allow tuning of temporal pulse profiles for mixed-metal applications.
What cutting speed can be expected when processing 30mm S355JR carbon steel with a 30kW fiber laser?
Using nitrogen assist gas at 20 bar pressure and a 2.0mm nozzle, a 30kW fiber laser can achieve a verified cutting speed of 4.2 m/min on 30mm S355JR carbon steel while maintaining an edge roughness of Ra ≤12.5µm suitable for direct welding.
Why is beam quality important when specifying fiber laser equipment for varying steel thicknesses?
Fiber laser systems with a beam quality of M²≤1.1 maintain consistent kerf geometry. This holds across varying material thicknesses. Without this specification, performance degrades predictably as section depth increases. This can fail precision requirements for structural fabrication.
Sources and further reading. Readers evaluating these solutions can verify the underlying requirements directly. The standards organisations below provide the details:
- ASTM International — ASTM Committee E07 nondestructive-testing standards and test methods.
- IEC — IEC standards for inspection instrumentation and electromagnetic compatibility.
- ISO — ISO 9712 NDT personnel qualification and ISO 16810 ultrasonic testing.