
Key Considerations in Minimizing the Heat-Affected Zone
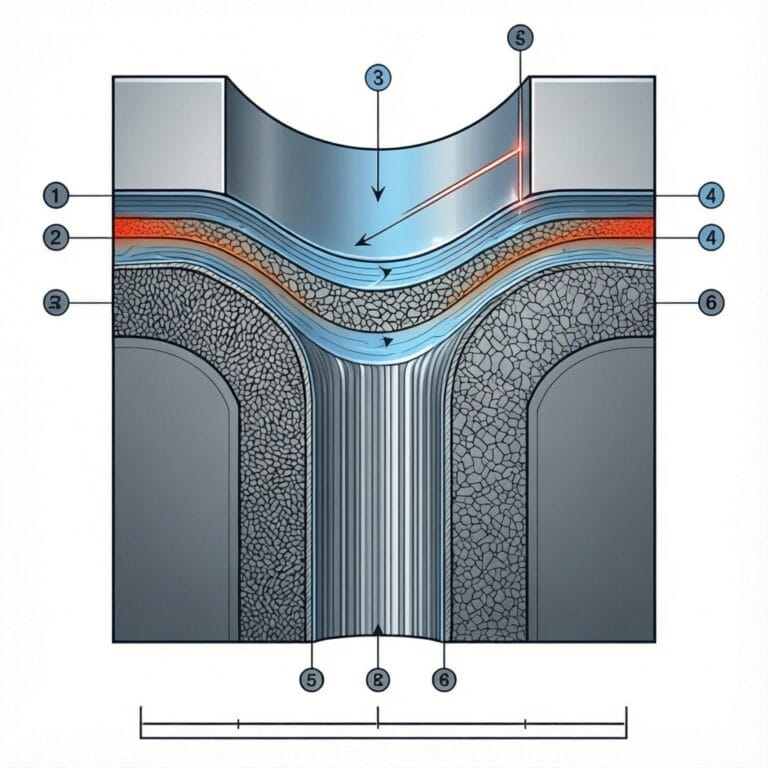
The heat-affected zone (HAZ) is the region of base material whose microstructure and properties are altered by welding heat — but not melted. In precision fabrication, controlling HAZ width and severity directly determines part quality, post-weld distortion, and whether secondary machining is required. For thin-gauge stainless steel (0.5–1.5mm) used in medical devices, electronics enclosures, and heat exchanger plates, HAZ width beyond 0.5mm can cause unacceptable warping that scrap the part.
Fiber laser welding at 1,064nm wavelength produces HAZ widths of 0.8–1.5mm in stainless steel, compared to 3–6mm for TIG welding. This 75–85% reduction occurs because the fiber laser’s concentrated energy density melts the joint with minimal lateral heat conduction — the surrounding material sees less total thermal energy per unit length of weld. Intouchray fiber laser systems achieve this through beam quality M² ≤ 1.1 and positioning accuracy of ±0.03mm.
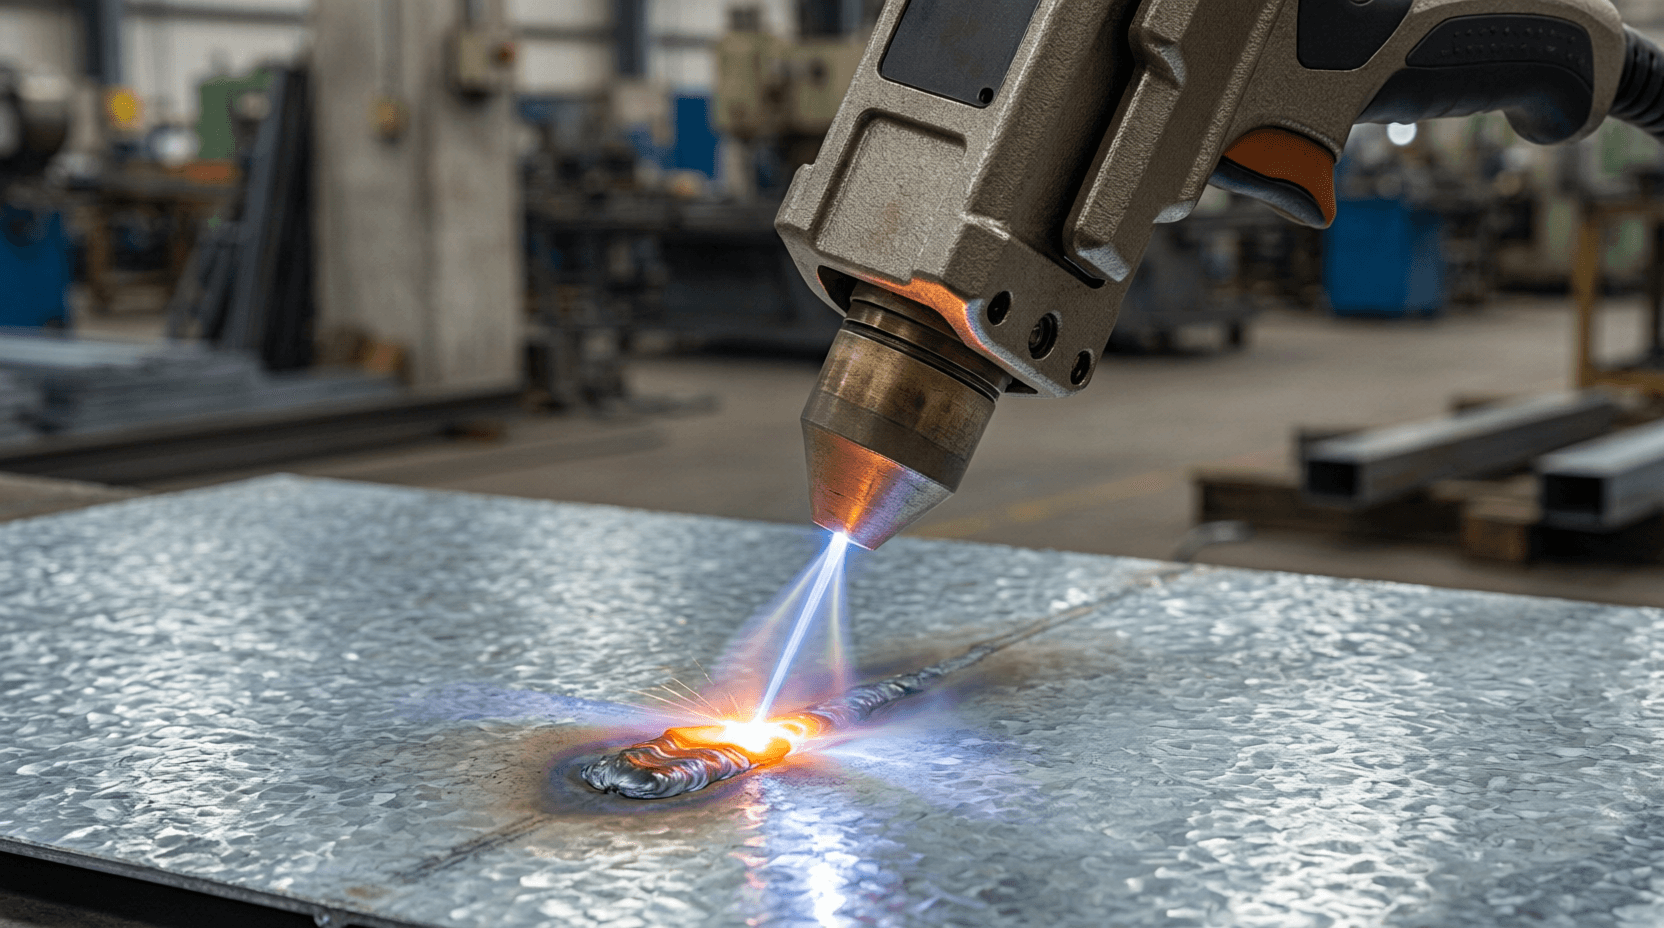
Power, Speed, and Material Compatibility: The HAZ Control Variables
Three parameters dominate HAZ formation: laser power, travel speed, and material thermal conductivity. Higher power enables faster travel speeds which reduce total heat input per unit length — the primary lever for HAZ minimization. But too much speed creates incomplete penetration; too little power requires slower travel which increases HAZ width.
Material thermal conductivity determines how quickly heat dissipates from the weld zone. Copper (401 W/m·K) pulls heat away so rapidly that achieving full penetration requires higher power, which in turn increases total heat input. The 1,064nm fiber laser wavelength is absorbed efficiently by copper — roughly 35% more than CO₂ at 10,600nm — which helps offset this challenge. Aluminum (237 W/m·K) presents a middle ground; stainless steel (16 W/m·K) retains heat locally, making HAZ control primarily a function of travel speed.
Technical Analysis: HAZ Control in Laser Welding
Pulse shaping — modulating laser power during each millisecond of the weld pulse — provides finer HAZ control than continuous wave (CW) welding. A typical pulse profile for 0.8mm 304 stainless steel uses a rapid ramp-up to peak power for penetration, a sustained mid-pulse plateau at reduced power for controlled melt pool growth, and a gradual ramp-down to minimize solidification rate at the weld toe — the region most susceptible to HAZ cracking.
Shield gas selection also affects HAZ. Argon provides superior arc stability and weld pool protection but has lower thermal conductivity than helium, which means more heat stays in the workpiece. Helium-argon mixtures (25–75% He) improve heat dissipation for thick sections or heat-sensitive alloys at higher gas cost. Nitrogen is occasionally used for duplex stainless steels but risks nitride formation in austenitic grades.
Industry Examples: Real Applications of HAZ Control
In thin-gauge electronics enclosures — where 0.5mm 316L stainless forms the housing for industrial control panels and outdoor-rated equipment — HAZ-induced warping is the primary rejection cause. A Guangdong fabricator using Intouchray’s 1.5kW fiber laser welder reduced post-weld straightening time from 12 minutes to under 2 minutes per enclosure by switching from micro-TIG, eliminating a secondary press operation that previously added 18% to per-unit labor cost.
In medical implantable device housings (titanium Grade 23, 0.8mm wall), HAZ must be kept below 0.3mm to preserve the material’s fatigue strength. The fiber laser’s pulse shaping capability achieves this through controlled solidification rates, while the autogenous process (no filler metal) eliminates the contamination risk that disqualifies TIG-welded medical components from ISO 13485 compliance audits.
Supplier Solution: Intouchray’s Engineering Approach
Intouchray fiber laser welding systems provide the parameter control necessary for HAZ-sensitive applications: beam quality M² ≤ 1.1, positioning accuracy of ±0.03mm, and pulse shaping capability across the full power range (500W to 6kW). Available laser sources — IPG, Raycus, MAX — allow buyers to match source reliability and service network to their geographic location.
For procurement managers evaluating HAZ-sensitive fabrication, Intouchray offers pre-purchase weld sample demonstrations. Submit your material specification (grade, thickness, joint geometry) to receive welded samples with micrographs showing HAZ width measurement — a direct comparison against your current process capability.
Frequently Asked Questions
What laser parameters minimize HAZ in stainless steel?
Higher travel speed with proportionally higher power minimizes total heat input per unit length — the primary HAZ driver. For 1mm 304 stainless, 1kW at 1.8 m/min typically produces HAZ under 1mm. Pulse shaping with controlled ramp-down further reduces HAZ at the weld toe by preventing excessive solidification time at peak temperature.
Does fiber laser or CO₂ produce less HAZ?
Fiber laser produces significantly narrower HAZ because the 1,064nm wavelength is absorbed more efficiently by metals than CO₂’s 10,600nm. Less energy is reflected or scattered, meaning more of the input power goes into the weld rather than heating surrounding material. The practical difference is 0.8–1.5mm HAZ for fiber versus 2–4mm for CO₂ on 1mm stainless steel.
Can HAZ be eliminated entirely?
No — any process that melts metal creates a HAZ. The goal is minimization to below the threshold that matters for the specific application. For most industrial applications, HAZ under 1.5mm is acceptable. For medical and aerospace, under 0.3mm is achievable with optimized fiber laser parameters and pulse shaping.
Industry Standards & References
Related Articles
- Fiber vs CO₂: Minimizing HAZ in Sensitive Alloys
- Welding Thin-Gauge Stainless Steel without Thermal Distortion