
Key Considerations in Laser Welding Optics Maintenance
The protective window — a transmissive optical element that sits between the focusing lens and the welding environment — is the single most frequently replaced consumable on a fiber laser welding system. It costs $30–150 depending on diameter and coating, but when it fails — through pitting, thermal cracking, or contamination buildup — it can destroy the focusing lens behind it, a $500–2,000 component. A disciplined window inspection and replacement schedule is the cheapest insurance policy in laser welding.
Contamination enters the optical path through three routes: weld fume and spatter ejected upward from the molten pool, airborne dust drawn into the nozzle by shield gas turbulence, and back-reflection from highly reflective workpieces that deposits vaporized material on the window surface. All three are normal parts of production; none indicate equipment malfunction. The maintenance question is not “how do I prevent contamination?” but “how frequently do I inspect and replace the window before contamination becomes damage?” Intouchray recommends inspection at the start of every shift and replacement when transmission loss exceeds 5%, as measured by the system’s built-in power calibration routine.
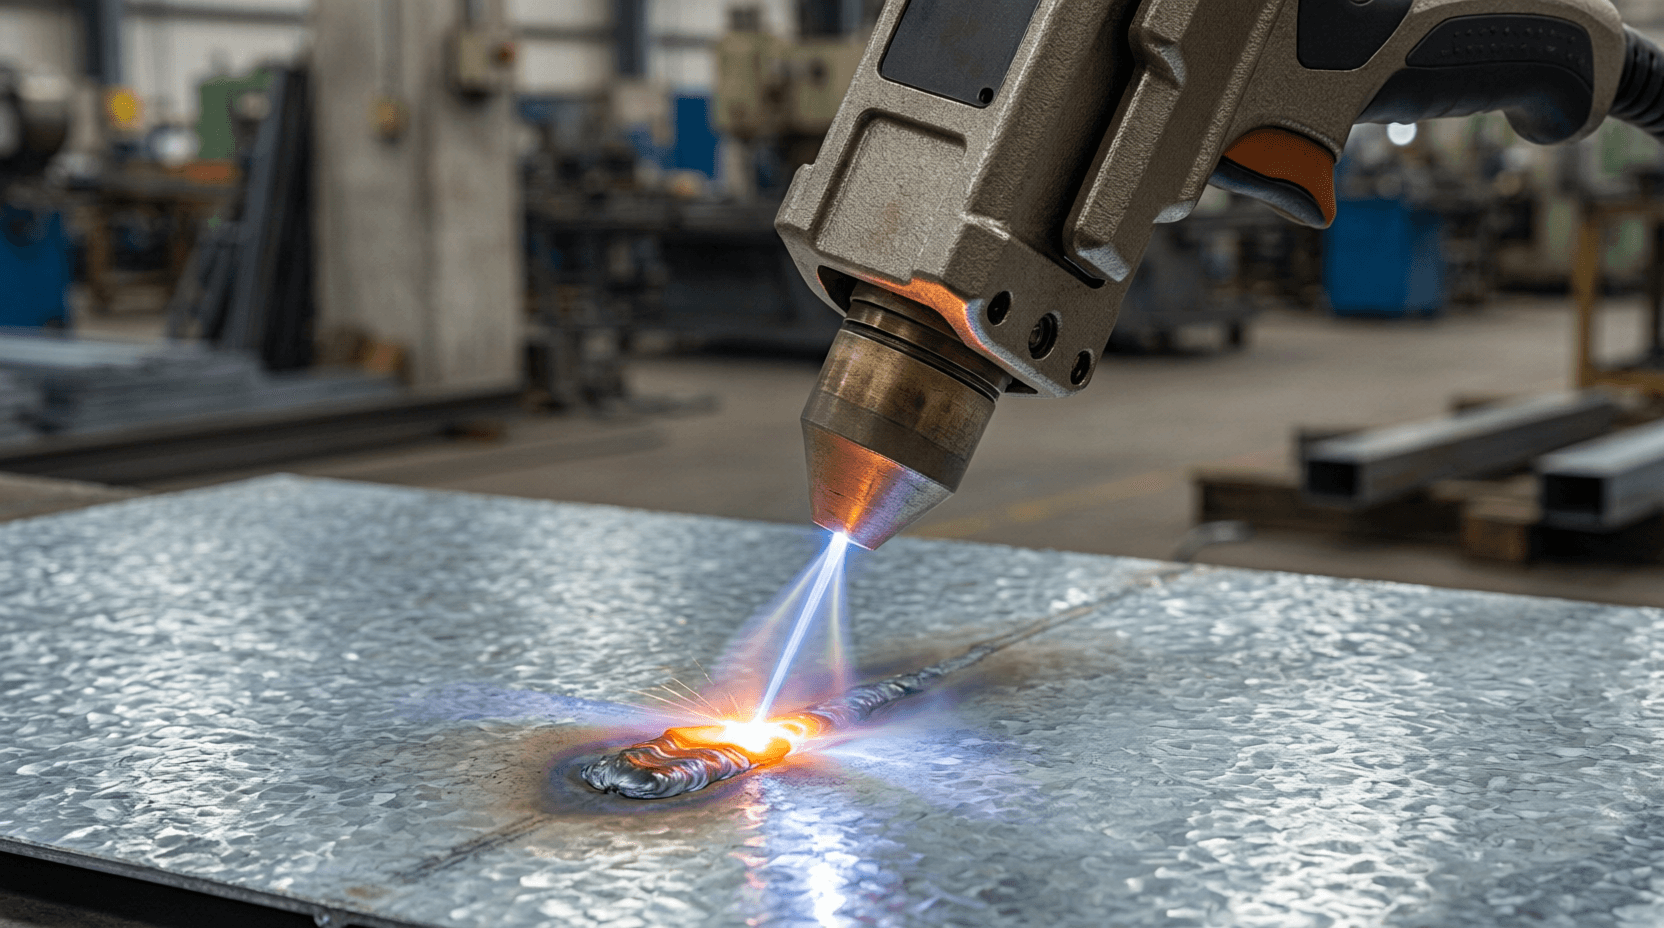
Daily, Weekly, and Monthly Inspection Schedule
| Frequency | Task | Tool/Check |
|---|---|---|
| Every shift | Inspect protective window for pits, cracks, discoloration | Visual inspection under bright light at oblique angle |
| Every shift | Check shield gas flow rate at nozzle | Flow meter — verify against procedure spec (typically 12–18 L/min) |
| Every shift | Clean nozzle tip of spatter deposits | Brass brush or nozzle reamer — never steel (scratches orifice) |
| Weekly | Inspect and clean focusing lens (if accessible) | Lens tissue + isopropyl alcohol — inspect under magnification |
| Weekly | Verify beam centering through nozzle | Transparent tape test — fire at low power, check burn mark centered |
| Weekly | Clean or replace chiller water filter | Visual — replace if discolored or flow restricted |
| Monthly | Full calibration check — power at workpiece vs. setpoint | Power meter — verify within ±2% of setpoint across power range |
| Monthly | Inspect all optical fiber connectors for contamination | Fiber inspection microscope — clean with one-shot connector cleaner |
| Monthly | Verify all safety interlocks and door switches | Functional test — attempt operation with each interlock opened |
Practical Implementation Notes
Window replacement procedure: Wear powder-free nitrile gloves — skin oils transferred to the window surface absorb laser energy and create hot spots that lead to thermal cracking. Remove the retaining ring with the supplied spanner wrench (never pliers — they distort the ring). Extract the old window by tipping the holder; do not pry with metal tools. Inspect the O-ring for compression set or cuts — replace if any doubt. Insert the new window with the coated side facing the laser source (typically marked with an arrow or dot). Torque the retaining ring to the system specification — over-tightening induces stress birefringence in the window, distorting the beam profile.
Spatter management: Weld spatter — droplets of molten metal ejected from the weld pool — deposits on the nozzle face, window, and surrounding hardware. A cross-jet air knife mounted between the nozzle and window deflects spatter away from the optical path. Verify cross-jet operation at the start of each shift — a clogged cross-jet nozzle provides zero protection and is worse than no cross-jet because it creates a false sense of security. Clean the cross-jet orifice weekly with a fine wire or solvent flush.
Intouchray’s Quality Assurance Support
Intouchray provides a comprehensive maintenance kit with each fiber laser welding system: spare protective windows (quantity based on expected monthly consumption at typical duty cycle), lens cleaning supplies, nozzle reaming tools, O-ring kit, and a maintenance logbook with inspection checklists. The system’s onboard diagnostics monitor protective window transmission and alert the operator when transmission drops below the 95% threshold — before the window degrades to the point of risking the focusing lens.
For production environments running multi-shift operations, Intouchray recommends maintaining a minimum 2-week supply of all consumables (windows, nozzles, O-rings, chiller filters) based on actual consumption tracking from the maintenance log. Running out of a $50 window with 200 parts due by Friday is a preventable production stoppage.
Frequently Asked Questions
How often should the protective window be replaced?
Inspect every shift. Replace when visual inspection reveals any pitting, cracking, discoloration, or spatter adhesion that cannot be cleaned — typically every 40–80 hours of arc-on time in clean production environments, or every 20–40 hours in high-spatter applications like galvanized steel welding. The system’s transmission monitoring provides an objective threshold: replace at 95% transmission or below.
What causes the protective window to crack during welding?
Thermal shock from a spatter droplet landing on the window surface creates a localized hot spot that expands faster than the surrounding material — the resulting stress cracks the window. The cross-jet air knife prevents most spatter from reaching the window; verify it is functioning before troubleshooting window cracking as a material defect. Other causes include over-tightened retaining rings inducing stress and back-reflection from highly reflective workpieces causing localized heating.