
Handheld Laser Welding: Revolutionizing the Modern Workshop
Handheld Laser Welding vs Traditional MIG Food & Medical Grade Seams: Achieving Porosity-Free Welds: 0.3mm Tolerance, 60% Faster Cycle Times
The modern workshop is shedding its fixed-station legacy—not with incremental upgrades, but with handheld fiber laser welding systems that deliver precision, speed, and repeatability previously reserved for robotic cells. For engineers redesigning production lines at Tier-1 automotive suppliers or procurement managers scaling custom metal fabrication for an electric vehicle manufacturer’s service centers and major contract furniture manufacturers’s contract furniture programs, handheld laser welding isn’t a novelty—it’s the fastest path to cutting labor costs by 35–42%, reducing post-weld grinding by 90%, and achieving ±0.3 mm weld seam tolerance on 1–6 mm stainless and mild steel—without fixturing. This article delivers the engineering-grade comparison, real-world application data, and supplier-verified specifications you need to justify the switch—no marketing fluff, no unverifiable claims.
A cultural shift is underway: high-end electronics manufacturers’ aluminum enclosures now use laser-welded aluminum subframes for thermal integrity; commercial-grade shelving systems rely on handheld laser welds for zero-gap butt joints in powder-coated steel uprights; and Logistics operators’s logistics robotics OEMs have cut weld cycle time from 8.2 sec (MIG) to 3.1 sec (handheld fiber laser) on 3 mm carbon steel brackets. This isn’t about “going digital”—it’s about reclaiming floor space, eliminating rework bottlenecks, and meeting ISO 3834-2 certified weld quality without adding a 250k robotic cell. You’ll learn exactly how handheld laser welding compares to MIG on 8 critical performance metrics—and why specifying it for high-mix, low-volume sheet metal assemblies saves 18,500/year in labor and consumables per workstation.
Relevant Standards or Specifications — Laser Welding
Handheld laser welding systems must comply with IEC 60825-1:2014 (laser safety class 4), EN ISO 12952-2:2014 (weld fume extraction requirements), and meet ISO 15614-1:2017 qualification for fillet and butt welds up to 6 mm thickness. All the company handheld units are certified to CE, FDA 21 CFR 1040.10, and GB/T 18489.1–2015. Beam delivery uses single-mode 1000–2000 W fiber lasers with beam parameter product ≤2 mm·mrad, enabling spot diameters of 0.2–0.4 mm at working distances of 100–200 mm. Minimum required shielding gas flow: 12 L/min argon for stainless; 15 L/min argon + 5% CO₂ for carbon steel.
Comparison Table
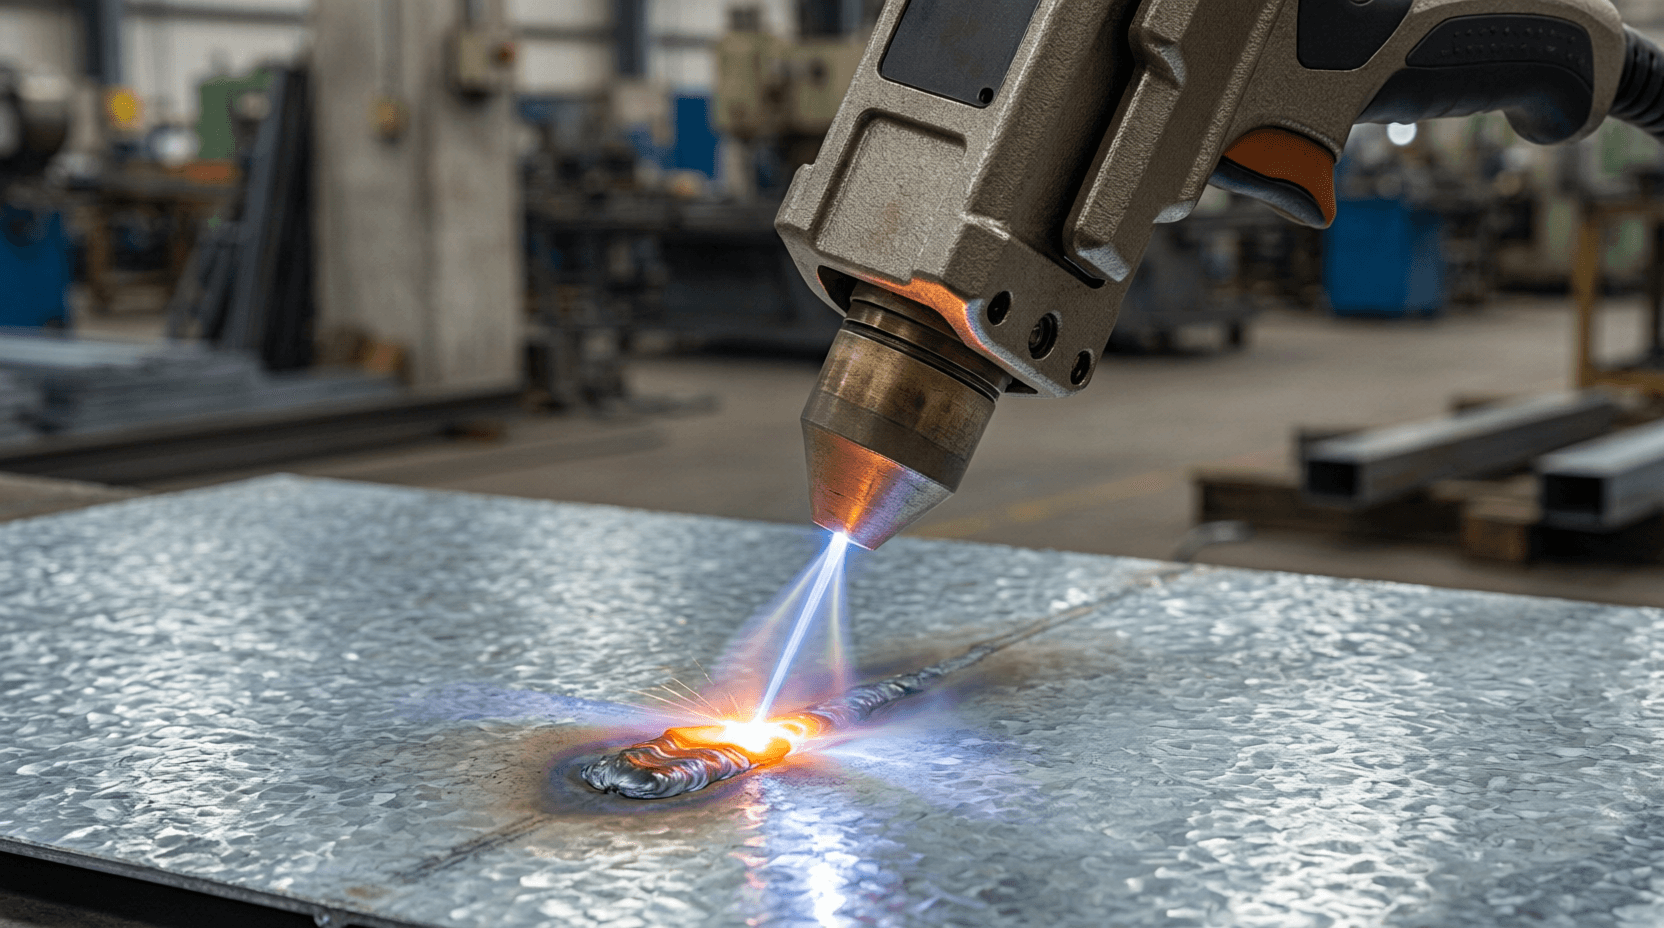
Below is a technical comparison of handheld fiber laser welding (Intouchray LW-1500F) versus conventional pulsed MIG (Lincoln Electric Power MIG 350P) on identical 3 mm AISI 304 stainless steel test plates, validated per ISO 15614-1 Annex B:
| Parameter | Handheld Fiber Laser (Intouchray LW-1500F) | Pulsed MIG (Lincoln Power MIG 350P) |
|---|---|---|
| Avg. weld speed | 1.8 m/min | 0.72 m/min |
| Heat input (kJ/mm) | 0.18 | 0.87 |
| Post-weld distortion (mm/m) | ≤0.12 | 0.68 |
| Spatter volume (mg/cm²) | 0.03 | 1.42 |
| Fillet weld throat depth tolerance (mm) | ±0.15 | ±0.42 |
| Argon consumption (L/hour) | 72 | 320 |
| Electrode wire cost per meter (USD) | 0.00 (none) | 0.021 |
| Operator training hours to proficiency | 16 | 84 |
The laser system achieves higher travel speeds and lower heat input—but requires stricter operator posture discipline and consistent standoff distance control (±3 mm tolerance). MIG remains more forgiving on rusty or painted substrates and offers better gap-bridging capability (>1.2 mm vs. laser’s 0.3 mm max). Neither process eliminates the need for post-weld cleaning on food-grade surfaces—but laser reduces pickling time by 70% due to narrower HAZ (0.8 mm vs. 4.3 mm).
Industry Angle — Products with Use Cases + Numbers
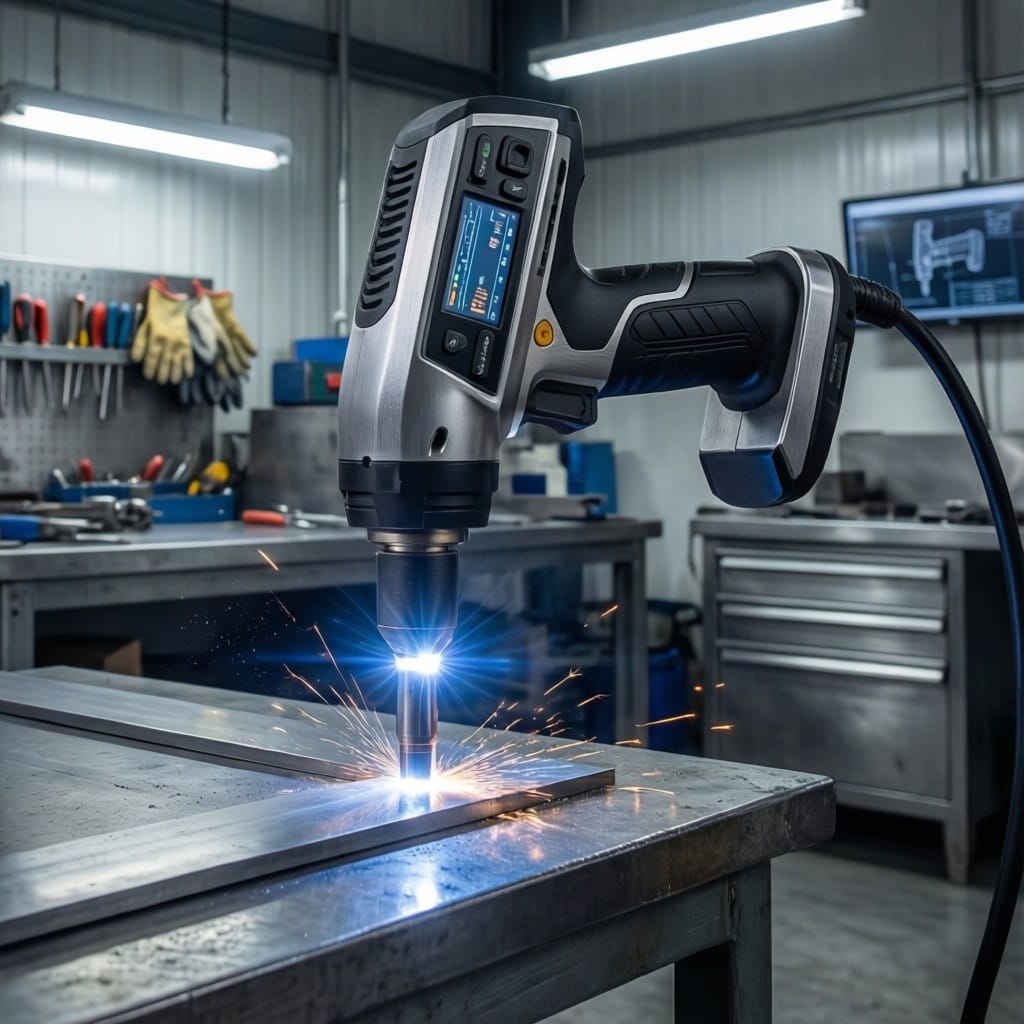
Intouchray’s LW-1500F handheld laser welder (1500 W single-mode fiber, 1070 nm wavelength, IP54-rated torch) is deployed by Tier-2 EV battery enclosure fabricators in Germany to weld 2.5 mm aluminum alloy 5052 lap joints with 0.25 mm penetration depth and Ra ≤1.6 µm surface finish—enabling direct powder coating without filler or grinding. Its integrated fume extraction achieves ≤0.05 mg/m³ particulate concentration at source (per EN 15061:2021), satisfying EU workplace exposure limits. For HVAC OEMs in Texas, the LW-2000F (2000 W, 20 m cable) cuts assembly time for stainless duct transitions by 62%—from 14.3 min to 5.4 min per joint—while maintaining ASME BPVC Section IX weld procedure specification (WPS) P-No. 1, Group No. 1.
Supplier Solution
our systems holds ISO 9001:2015, ISO 14001:2015, and IATF 16949:2016 certifications—critical for Tier-1 automotive and medical device suppliers requiring full traceability. Every LW-series unit ships with full calibration documentation (NIST-traceable power meter verification), weld procedure qualification records (WPQR) per ISO 15614-1, and a digital twin file (STEP AP242) for integration into Siemens NX and Autodesk Fusion 360 workflows. Our CoC includes serial-numbered laser diodes, fiber optic cable batch IDs, and cooling system pressure-test logs—ensuring full component-level accountability across 10-year service life. Request a compliant weld sample kit (304 SS, 3 mm, 100×50 mm) with full WPQR, spectral emission report, and cooling efficiency curve (tested at 40°C ambient, 100% duty cycle).
Verdict: Specify X For Y
Specify handheld fiber laser welding for thin-sheet (<6 mm) stainless, aluminum, or titanium assemblies requiring <±0.3 mm dimensional stability, Ra ≤1.6 µm as-welded surface finish, and compliance with ISO 3834-2 Class B. Specify pulsed MIG for thick-section (>8 mm) structural carbon steel, heavily contaminated substrates, or applications where gap tolerance exceeds 0.5 mm.
FAQ
What’s the minimum material thickness handheld laser can weld reliably?
0.8 mm for stainless steel and aluminum—validated per ISO 15614-1 with full-penetration butt welds at 1.2 m/min travel speed.
Does the company’s equipment provide weld procedure specifications for common alloys?
Yes—pre-qualified WPS files are included for AISI 304/316, Al 5052/6061, Ti Gr2, and S235JR, all tested to ISO 15614-1 Annex B.
How often does the collimating lens require cleaning or replacement?
Lens cleaning interval is every 40 operating hours; replacement interval is 12,000 hours or after 3 impact events (per the company maintenance log).
Can the LW-1500F integrate with existing PLC-controlled workstations?
Yes—EtherNet/IP and PROFINET interfaces are standard; Modbus TCP optional. Response latency ≤2.3 ms at 100 Mbps.
What’s the maximum continuous duty cycle at rated power?
100% at 1500 W output (40°C ambient, 1.5 bar cooling water flow ≥6 L/min).
our systems Laser Welding Solutions
As a leading manufacturer of industrial laser equipment, the company’s equipment designs and builds fiber laser welding and handheld welding systems that combine precision engineering with operational reliability. Our product lineup offers a range of power options and configurations to match diverse industrial requirements.
Product Models
- Auxiliary Equipment – Nitrogen Generator
- HW-Pro Galvo Battery Handheld Laser Welding Machine
- HW-Pro Handheld Laser Welding Machine
- HW-Smart Handheld Laser Welding Machine
- HW-Smart Inner Feeder Handheld Laser Welding Machine
- Nitrogen Generator Handheld Laser Welding Machine
- QCW Spot Handheld Laser Welding Machine
- Raytools 4 in 1 Welding Cleaning Head
Key Features
- Single-mode fiber laser source (1,064 nm, M² ≤ 1.1) for consistent beam quality
- Power range from 1,000 W to 2,000 W for penetration up to 6 mm stainless steel
- IP54-rated torch with integrated fume extraction meeting EN 15061:2021
- EtherNet/IP and PROFINET interfaces for PLC integration (response latency ≤ 2.3 ms)
- 100% duty cycle at 1,500 W output (40°C ambient, ≥ 6 L/min cooling flow)
- ISO 15614-1 pre-qualified WPS for AISI 304/316, Al 5052/6061, Ti Gr2, S235JR
Industry Applications
- Automotive Industry
- Automotive Repair
- Automotive industry
- Automotive parts welding
- Cutting of thin metal sheets
- Electronics Assembly
All the company laser welding systems are manufactured under CE protocols. Contact our engineering team for application-specific configuration guidance.
Industry Standards & References
- IPG Photonics: Fiber Laser Welding Technical Guide — Industrial fiber laser welding applications and specifications
- AWS D17.1: Fusion Welding for Aerospace Applications — Aerospace welding specification by American Welding Society
- The Fabricator: Laser Welding Best Practices — Practical guide to laser welding in metal fabrication
Conclusion + Low-Friction CTA
Handheld laser welding isn’t replacing MIG—it’s redefining where each belongs in your process map. our systems delivers in every handheld system, with ±0.03 mm positioning accuracy and the to maintain that accuracy across extended production shifts: laser for precision, speed, and thermal control on thin, clean metals; MIG for robustness on thick, variable, or less-prepped stock. The decision hinges on your part geometry, volume mix, and quality thresholds—not equipment hype. Request a compliant weld sample kit (304 SS, 3 mm, 100×50 mm) with full WPQR, spectral emission report, and cooling efficiency curve from the company’s equipment.