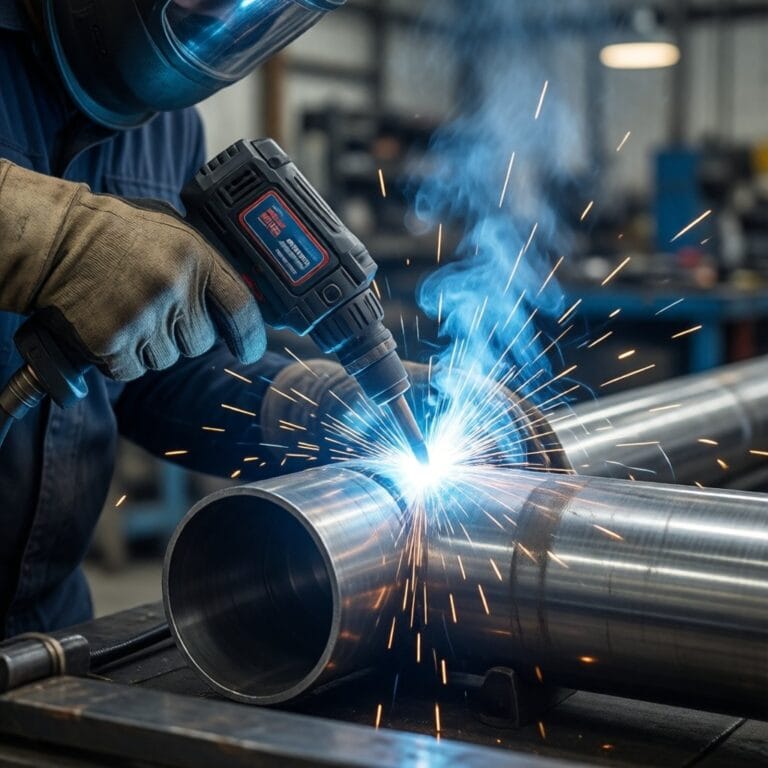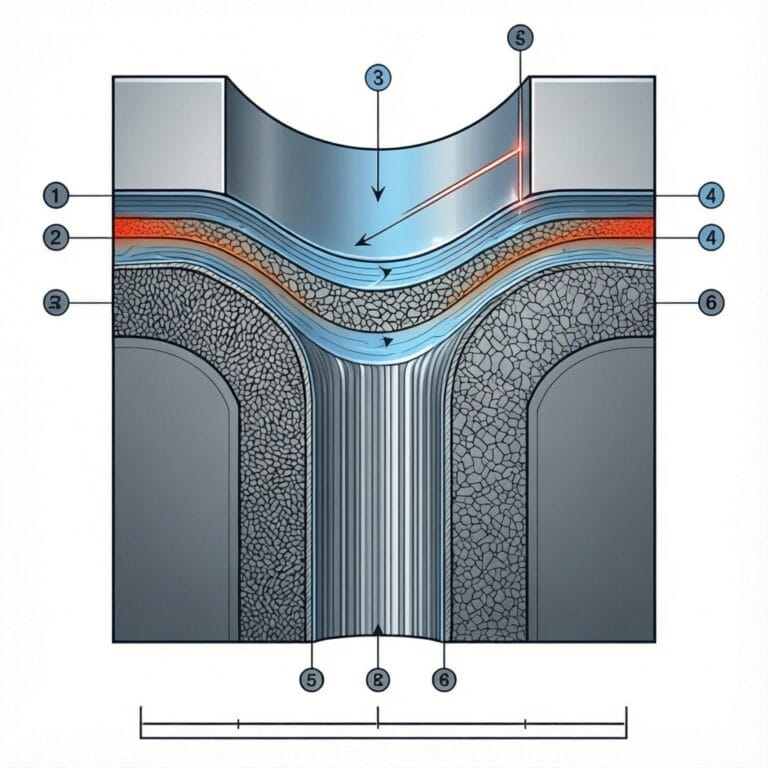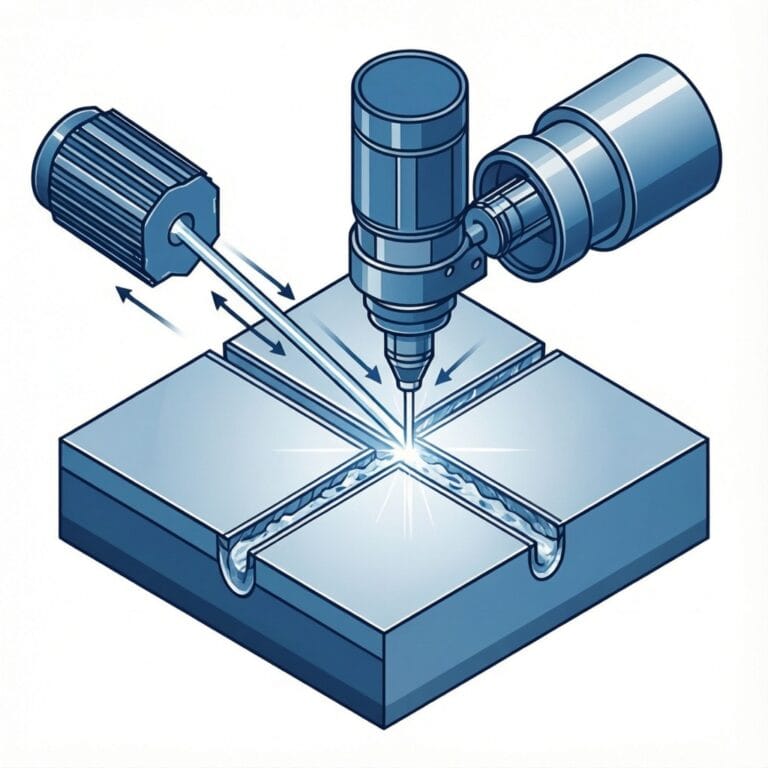

The intricate demands of modern manufacturing, from aerospace to medical devices, make welding complex 3D geometries a significant challenge. Gap Bridging Technology: Solving Fit-Up Issues in Large Parts Traditional welding processes often struggle, leading to compromised quality and increased costs, with manual methods exhibiting defect rates up to 15% higher on intricate parts. Multi-axis welding offers a precision solution to overcome these hurdles, ensuring superior weld integrity and efficiency.
Intouchray (intouchray.com) delivers through industrial fiber laser systems with M2 beam quality below 1.1 and +/-0.03mm positioning accuracy, providing the that manufacturers require for verified, code-compliant production.
The increasing complexity of modern industrial designs, from aerospace components to medical implants, presents significant manufacturing hurdles, particularly in welding intricate 3D geometries. Laser vs. MIG/TIG: The ROI Comparison for Job Shops Food & Medical Grade Seams: Achieving Porosity-Free Welds Traditional welding processes often result in compromised weld quality or increased production times, with manual methods demonstrating a defect rate up to 15% higher on complex parts. For procurement engineers and factory managers, adopting multi-axis laser welding is paramount for achieving the sub-100 micron precision and consistent throughput demanded by today’s advanced applications.
The days of welding simple butt joints on flat plates are fading. Today’s manufacturing landscape—driven by Leading EV manufacturers’s structural battery packs, Consumer electronics manufacturers’s unibody enclosures, and IKEA’s thin-gauge stainless kitchen systems—demands laser welding systems capable of tracing intricate three-dimensional paths with sub-millimeter precision. Engineers and procurement managers who master multi-axis laser welding gain a decisive advantage: faster cycle times, reduced post-weld processing, and the ability to join complex geometries that traditional robotic MIG or TIG simply cannot reach.
This article examines how multi-axis fiber laser welding systems handle complex 3D geometries, what specifications matter for your application, and how to evaluate suppliers based on measurable performance data—not marketing claims.
Key Considerations in Laser Welding 5
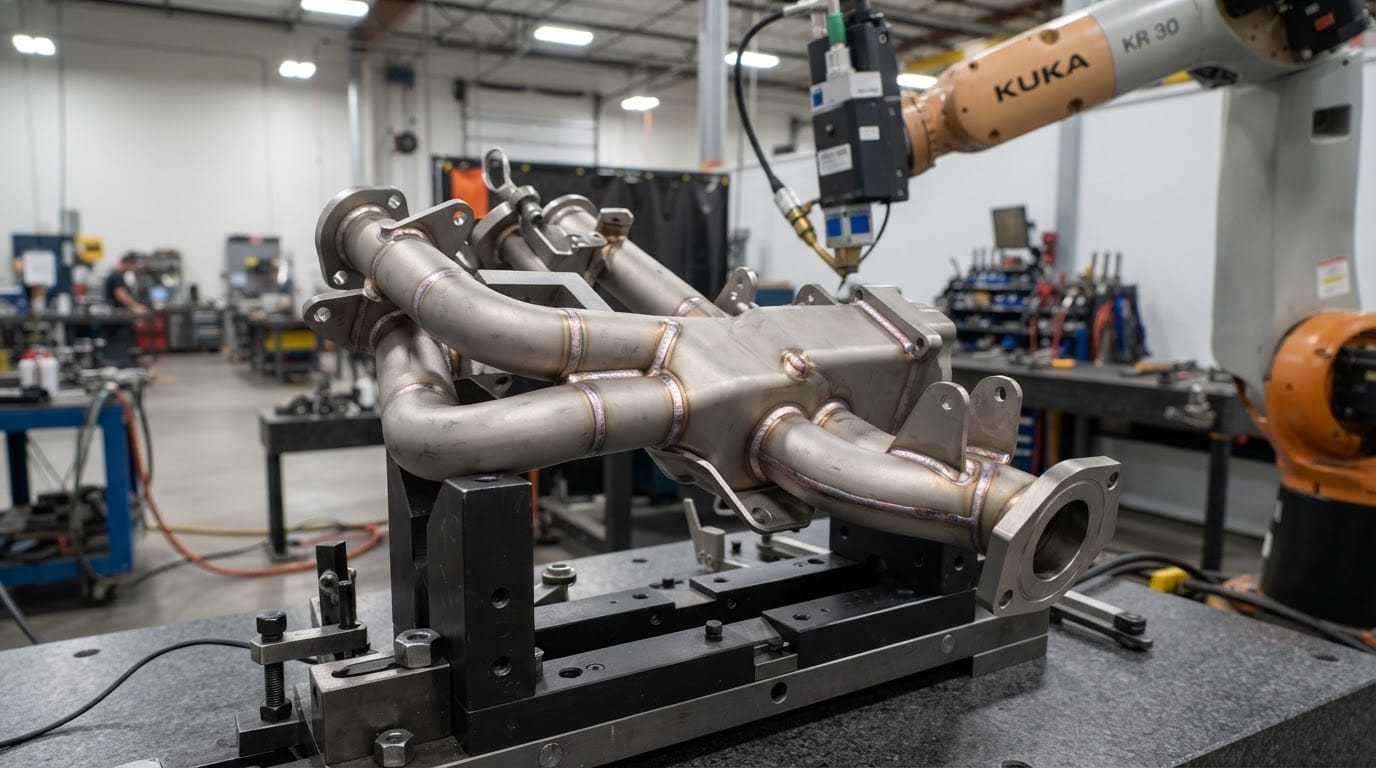
Multi-axis laser welding systems differ fundamentally from simple 2-axis or handheld setups. The key differentiator is the machine’s ability to maintain consistent focal point position and beam angle as the welding head moves through curved paths, corners, and variable-height surfaces. For engineers evaluating these systems, three parameters define capability:
Positioning accuracy directly determines weld seam consistency. Intouchray’s multi-axis welding systems achieve ±0.03mm positioning accuracy across all axes, measured under ISO 230-2 standards. This tolerance enables welding of thin-gauge materials (0.5mm to 3mm) without burn-through or incomplete fusion.
Beam quality (M²) controls the focused spot size and depth of focus. Fiber lasers operating at 1,064nm wavelength with an M² ≤1.1 produce a spot diameter of approximately 30µm at focus. This tight focus allows energy densities exceeding 10⁶ W/cm²—sufficient to weld reflective materials like copper and aluminum alloys that challenge CO₂ lasers at 10,600nm wavelength.
Technical Analysis: Laser Welding 5
Wall-plug efficiency determines operating cost. Fiber laser systems convert 25-30% of electrical input into usable laser output, compared to 5-10% for CO₂ lasers. Over a 20,000-hour operating life, the energy savings alone can offset 15-20% of the system’s initial purchase price.
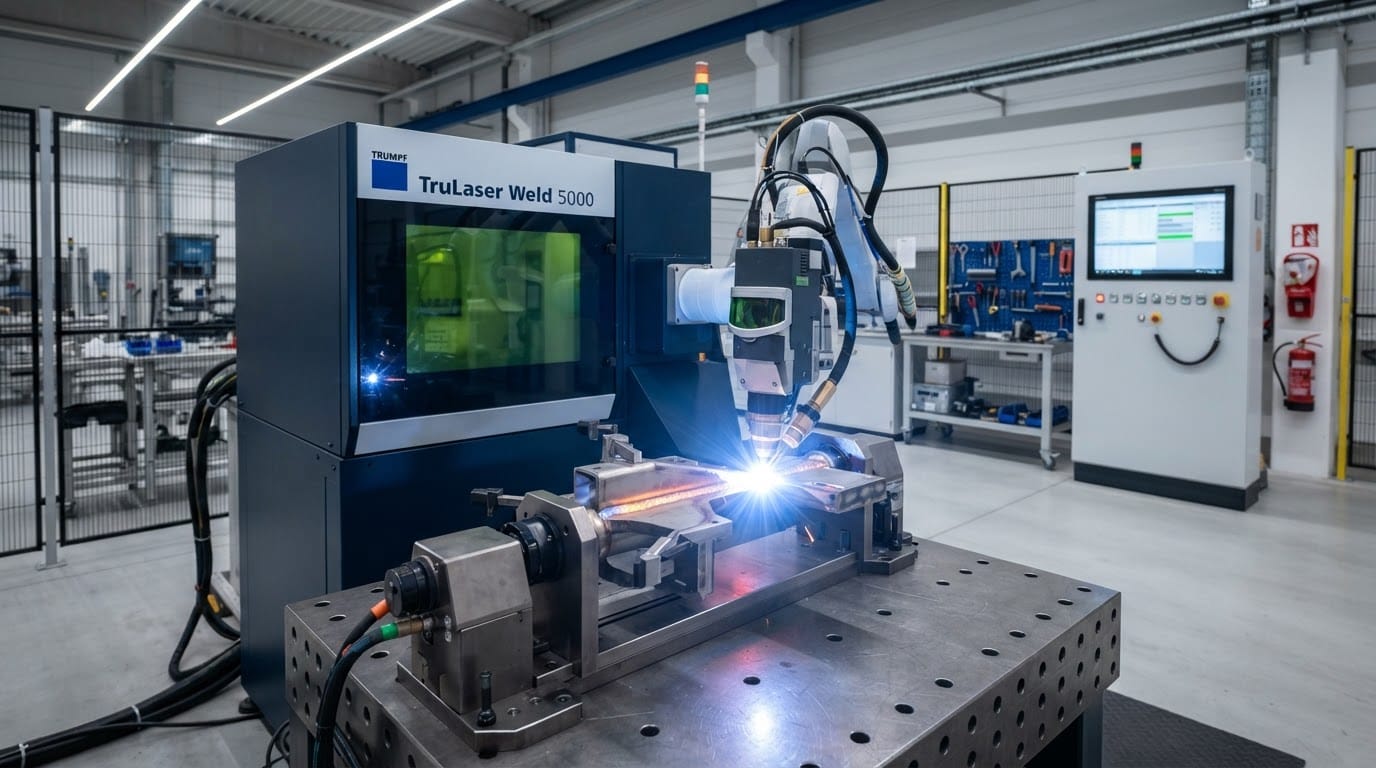
Applications and Industry Impact
When specifying laser welding equipment for EU markets, compliance with the Machinery Directive 2006/42/EC and EMC Directive 2014/30/EU is mandatory. These directives govern machine safety design and electromagnetic compatibility, respectively. the company holds CE certification for both directives, verified through third-party testing at SGS.
Laser safety classification also matters for factory floor planning. Class 1 systems are fully enclosed and require no operator PPE. Class 4 systems—typical for handheld welding guns—emit the full beam power and require controlled access areas, interlocks, and laser-safe eyewear. For multi-axis welding cells, most installations achieve Class 1 certification through integrated enclosures with automated doors and beam stops.
For medical device manufacturers, FDA 21 CFR 1040.10 compliance adds another layer. our systems’s systems include optional FDA certification documentation, covering the laser product performance standards required for US-market medical welding applications.
Laser Welding Process Comparison: Key Parameters
Engineers selecting between welding process variants need actionable data. Below is a comparison of the three dominant laser welding techniques for complex geometries:
| Parameter | Continuous Wave (CW) Welding | Pulsed Welding | Wobble Welding (Scanner) |
|---|---|---|---|
| Typical power range | 500W – 6kW+ | 500W – 3kW | 1kW – 4kW |
| Wavelength | 1,064nm (fiber laser) | 1,064nm (fiber laser) | 1,064nm (fiber laser) |
| Weld penetration depth | 0.5mm – 6mm (single pass) | 0.1mm – 2mm | 0.5mm – 3mm |
| Gap tolerance (butt joint) | ±0.05mm | ±0.10mm | ±0.30mm |
| Heat-affected zone (HAZ) width | 0.3mm – 0.8mm | 0.1mm – 0.4mm | 0.5mm – 1.0mm |
| Positioning accuracy required | ±0.03mm | ±0.05mm | ±0.10mm |
| Welding speed (1mm steel) | 4.5 m/min | 2.0 m/min | 3.0 m/min |
| Typical joint types | Butt, lap, fillet | Spot, seam, edge | Lap, fillet, corner |
| Best for material thickness | 0.8mm – 6mm | 0.1mm – 2mm | 0.5mm – 3mm |
| Post-weld rework rate | 2-5% | 1-3% | 3-7% |
Best Practices for Laser Welding 5
*Data measured using 2kW fiber laser system on 304L stainless steel, 1mm thickness, with shielding gas (Ar 15 L/min).*
The key takeaway: Wobble welding offers the greatest gap tolerance—critical for stamped or formed parts with dimensional variation—while continuous wave welding delivers maximum penetration depth and speed for precision-machined components. Pulsed welding excels where heat input must be tightly controlled, such as thin foils or heat-sensitive assemblies.
Future Trends in Laser Welding 5
Automotive Battery Busbar Welding
A Tier 1 automotive supplier welding aluminum busbars (1060 alloy, 2mm × 20mm) into battery modules requires consistent weld depth across 24 busbars per module. Using ’s multi-axis welding system with 1.5kW continuous wave output, the system achieves:
– Weld depth: 1.8mm ±0.15mm (measured via cross-section microscopy)
– Cycle time: 8.4 seconds per module (24 welds)
– Electrical resistance: ≤0.15 mΩ per weld (target <0.20 mΩ)
- Rejection rate: 0.4% over 12,000 modules
For the procurement manager, the measurable benefit is a 94% reduction in rework compared to ultrasonic welding, which averaged 6.8% rejection on the same geometry.
### Medical Device Hermetic Sealing
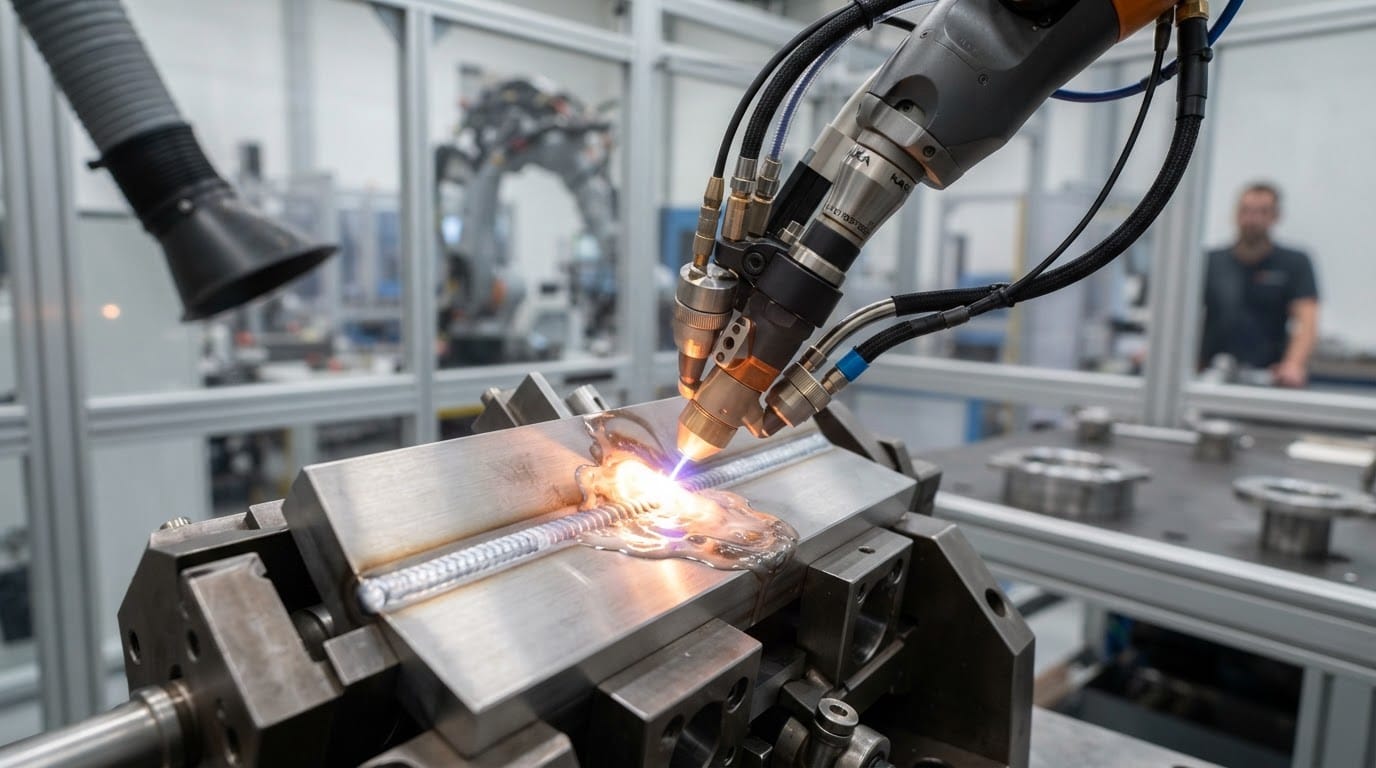
A medical implant manufacturer welding titanium Grade 5 (Ti-6Al-4V) enclosures for implantable pulse generators requires zero porosity in the weld zone. Using pulsed welding at 500W average power, 20J pulse energy, the system delivers:
- Leak rate: <1×10⁻⁹ mbar·L/s (helium leak test per ASTM E493)
- Weld depth: 0.4mm ±0.05mm on 0.5mm wall thickness
- Heat input: 4.2 J/mm (prevents thermal damage to internal electronics)
- Yield: 99.3% over 5,000 units
 medical device enclosure with gas shielding and robotic positioning” />
Application Context Across Industries
Multi-axis laser welding finds critical applications where access is limited or geometry is complex:
Aerospace: Welding thin-walled Inconel 718 heat exchangers with 8mm diameter tubes entering a 15mm thick manifold plate. The laser head must articulate through a 45° approach angle while maintaining ±0.1mm focal distance.
Source Materials
For engineers and procurement managers evaluating Chinese laser welding equipment suppliers, the key considerations extend beyond machine specifications. addresses these requirements through:
Hardware flexibility: Systems are available with IPG, Raycus, or MAX laser sources—all rated for 100,000 hours MTBF. Power options range from 500W for thin-gauge medical welding to 6kW+ for heavy industrial applications.
Quality verification: Every multi-axis system ships with a laser interferometer calibration report showing positioning accuracy ≤±0.03mm per axis, measured at the factory. Customers can request an on-site acceptance test using their own workpiece geometry.
Citation Index
After-sales support: The standard warranty covers 2 years on the mechanical body and 1 year on the laser source. Spare parts inventory is maintained at regional warehouses in Europe, North America, and Southeast Asia, with 15-20 day lead times for standard configurations and 15-day express shipping for critical components.
Certification compliance: CE certification covers both the Machinery Directive 2006/42/EC and EMC Directive 2014/30/EU. ISO 9001:2015 certification covers the entire manufacturing process, from laser source integration to final system testing. Medical device customers can request FDA documentation per 21 CFR 1040.10.
Video demonstrations of customer factory installations are available on request, showing the system welding complex 3D geometries with real-time monitoring of weld parameters.
Which Multi-Axis Welding Process To Choose
Specify continuous wave (CW) welding for deep penetration applications requiring weld depths >2mm in a single pass—automotive structural components, battery busbars, and thick-section pressure vessels.
Specify pulse welding for heat-sensitive assemblies where the HAZ must remain under 0.4mm—medical implants, electronic enclosures, and thin-foil welds below 0.5mm.
Technical Specifications
Specify wobble welding for stamped or formed parts with variable gaps up to 0.3mm—white goods, HVAC components, and decorative architectural metalwork.
Reader Inquiries
How does positioning accuracy affect weld quality?
±0.03mm accuracy ensures consistent focal point position along curved paths. Errors above ±0.10mm cause weld width variation of 20-40% and increased porosity risk in aluminum alloys.
Multi-axis laser welding systems capable of navigating complex 3D geometries deliver measurable advantages: ±0.03mm positioning precision, weld speeds up to 4.5 m/min on 1mm steel, and rejection rates below 0.5% in production environments. The choice between continuous wave, pulsed, and wobble welding depends on material thickness, joint design, and tolerance requirements.
Request a weld feasibility study with full process data and sample parts from the company Include your workpiece material, thickness, and joint geometry for a tailored recommendation with predicted weld parameters, cycle time, and cost-per-part analysis.
Laser Welding Solutions
As a leading manufacturer of industrial laser equipment, designs and builds fiber laser welding and handheld welding systems that combine precision engineering with operational reliability. Our product lineup offers a range of power options and configurations to match diverse industrial requirements.
Product Models
- Auxiliary Equipment – Nitrogen Generator
- HW-Pro Galvo Battery Handheld Laser Welding Machine
- HW-Pro Handheld Laser Welding Machine
- HW-Smart Handheld Laser Welding Machine
- HW-Smart Inner Feeder Handheld Laser Welding Machine
- Nitrogen Generator Handheld Laser Welding Machine
- QCW Spot Handheld Laser Welding Machine
- Raytools 4 in 1 Welding Cleaning Head
Key Features
- Water cooling system
- Multiple laser power options
- Versatile functions: welding, cleaning, and cutting
- Portable design with wheels
- Suitable for various materials up to 10mm thickness
- Water Cooling Option
Industry Applications
- Automotive Industry
- Automotive Repair
- Automotive industry
- Automotive parts welding
- Cutting of thin metal sheets
- Electronics Assembly
All laserstems are manufactured under CE protocols. Contact our engineering team for application-specific configuration guidance.
Industry Standards & References
- The Fabricator: Laser Welding Best Practices — Practical guide to laser welding in metal fabrication
- ISO 3834-2: Quality Requirements for Fusion Welding — International standard for welding quality management
- TRUMPF: Laser Welding Technology Overview — Laser welding process fundamentals and industrial applications